NIST’s Looping Laser Paths Improve Alloy Mixing, but Qualification Remains Open
Researchers at the National Institute of Standards and Technology have developed custom software that sends a metal 3D printer’s laser through looping paths, stirring the molten pool more effectively than conventional straight scans. In work described in the journal Additive Manufacturing with no publication date specified the team demonstrated improved mixing at the boundary between the dense refractory high-entropy alloy RHEA-19 and a lightweight titanium alloy. X-ray diffraction and electron microscopy confirmed better mixing and alloy formation, but no mechanical-property, production-scale or qualification data were reported.

The distinction matters for demanding U.S. aerospace and nuclear manufacturing. Demonstrating that two feedstock regions mix more uniformly is an important process result, especially when their constituent metals melt, flow and solidify differently. It does not yet establish tensile strength, fatigue life, fracture toughness, creep resistance or environmental durability. Those properties, along with repeatable production across machines and powder lots, would determine whether this method can progress from a materials experiment to critical hardware.
Laser motion becomes a melt-pool control input
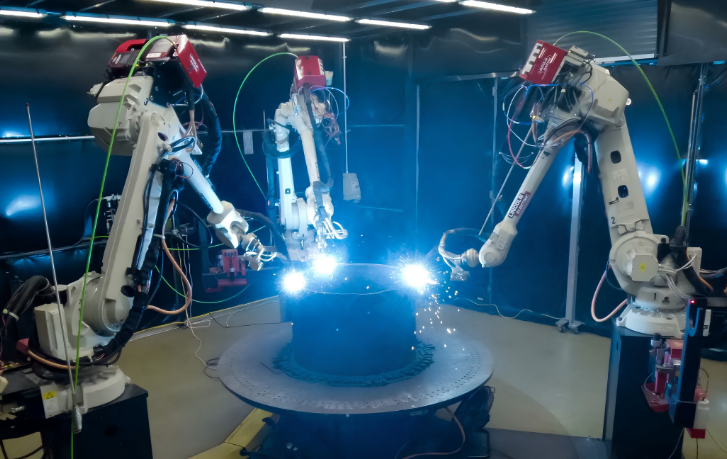
Laser powder bed fusion normally builds a component by scanning a focused laser over successive layers of metal powder. NIST’s intervention changes the path rather than adding printer hardware: the beam follows loops that induce greater motion in the liquid metal before it freezes. Researcher Ho Yeung’s team had to write the path-generation software from scratch because commercial printer software could not produce the required patterns.
The approach targets a central difficulty in processing high-entropy alloys. Unlike conventional alloys organized around one dominant base metal, these materials contain several metals in roughly equal proportions. NIST physicist and project co-leader Fan Zhang said they need mixing at the atomic level. That is difficult because each constituent can have different melting, flow and cooling behavior, creating opportunities for segregation during rapid solidification.
The relevant mechanism is liquid flow within the melt pool, not simply additional time for solid-state diffusion. Separate high-speed synchrotron work on copper and aluminum found that melt-pool flow dominated composition development and that mixing occurred through discrete events rather than smooth blending. That research also connected changing composition with keyhole stability and pore formation, illustrating why readers should treat mixing and defect control as coupled problems rather than independent settings. The Paul Scherrer Institute’s account of that work provides useful context for the underlying melt-pool physics.
Bright X-rays exposed rapid solidification behavior
NIST tested the process at Argonne National Laboratory’s Advanced Photon Source near Chicago. Its X-ray beams were described as roughly 500 billion times brighter than dental-office X-rays, providing the intensity needed to observe changes during rapid melting and solidification. Zhang called it one of the few photon sources powerful enough for this type of measurement.
X-ray diffraction and subsequent electron microscopy supplied complementary confirmation. Diffraction can identify crystal structures and phases, while microscopy can resolve local microstructure and compositional distribution. Together, these measurements supported the conclusion that laser stirring improved mixing and alloy formation across the RHEA-19 and titanium-alloy boundary. The reported work did not quantify how that change affected porosity, residual stress, grain orientation or mechanical performance.
Software compatibility does not equal industrial readiness
A software-defined method has an obvious integration advantage: it may avoid a new laser source, recoating system or printer architecture. Existing machines could potentially adopt the technique through software changes. However, that potential depends on whether their scan controllers can reproduce the loops with sufficient positional accuracy, timing consistency and synchronization with laser power. The team’s need for custom software shows that current commercial path-planning tools are not automatically ready for the method.
Qualification would also require a stable process window. Manufacturers would need to determine how loop geometry interacts with beam power, scan speed, layer thickness, powder condition and thermal history. Repeated builds would have to show that improved mixing persists across the full build volume and does not purchase compositional uniformity at the cost of pores, distortion or unstable melting.
NIST researchers ultimately envision printers combining elemental or basic metal powders on demand and changing alloy composition within one component, potentially including a turbine blade. Those are proposed applications, not demonstrated outcomes. No jet-engine or reactor component was reported as produced, certified or deployed, and no cost saving was established.
The immediate engineering result is narrower but still useful: laser trajectory can serve as an active control over melt-pool mixing, and NIST verified that effect with diffraction and microscopy. For critical U.S. applications, the next decisive evidence must come from repeatable builds and property testing. Better mixing is the process mechanism; durable, inspectable and certifiable material is the required product.
By Edward Collins — Senior editor for AMI’s performance systems and mechanical design coverage, focused on powertrains, drivetrain systems, manufacturing precision, materials, and high-performance engineering.